Benefits of Project
- Consistent and repeatable machine operation
- Fast fault location through diagnostics and alarm history
- Wiring simplified by distributed I/O close to the equipment
- Logic changes possible without rewiring the panel
- A platform with long term spare part and support availability
- Distributed I/O that cuts field wiring dramatically
- Diagnostics down to the individual channel
- Program structured so changes stay safe
Technologies We Used
- Siemens SIMATIC S7-1200 and S7-1500 controllers
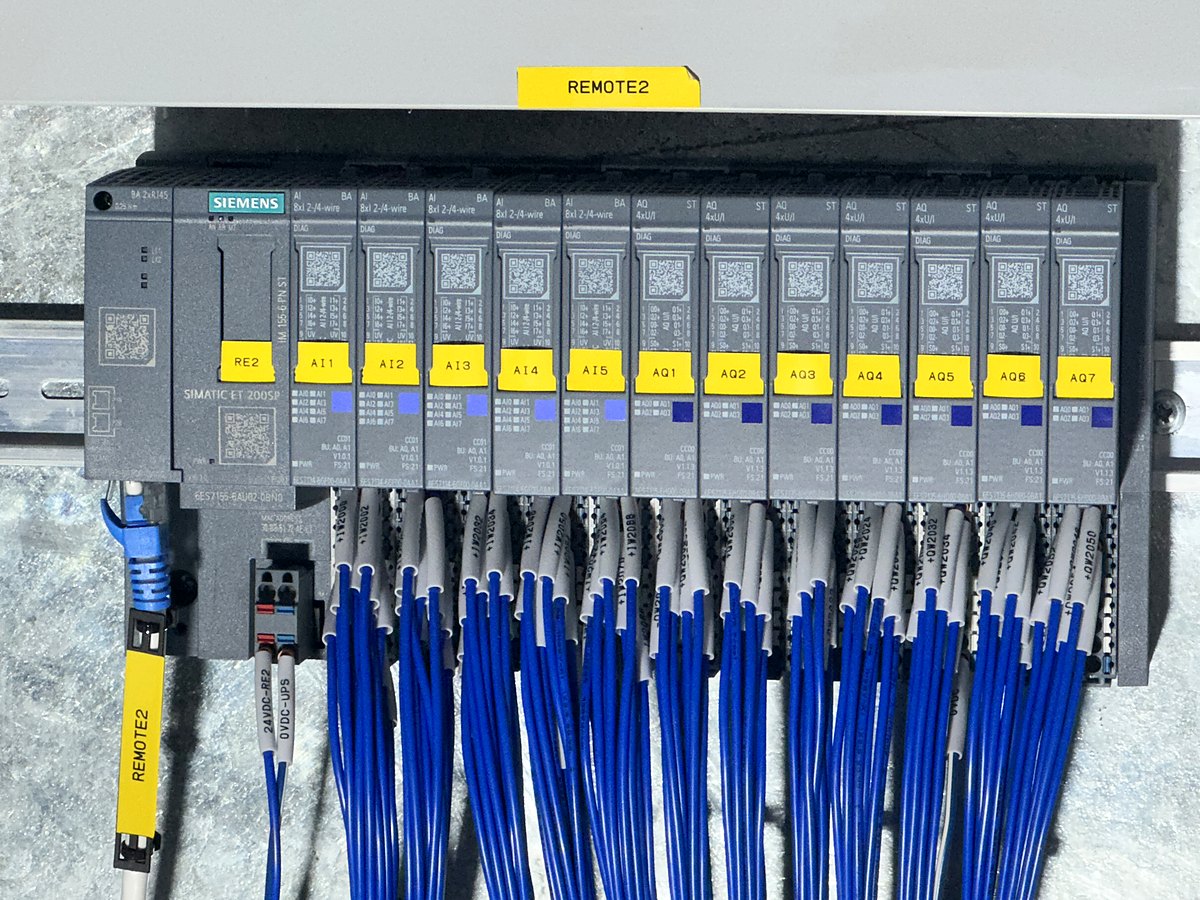
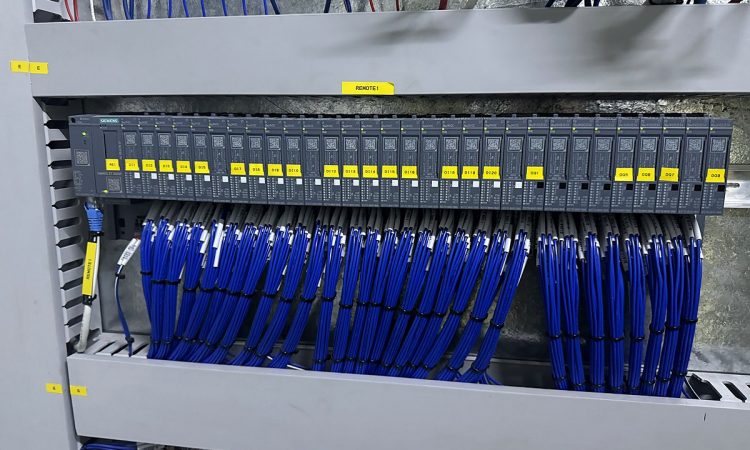
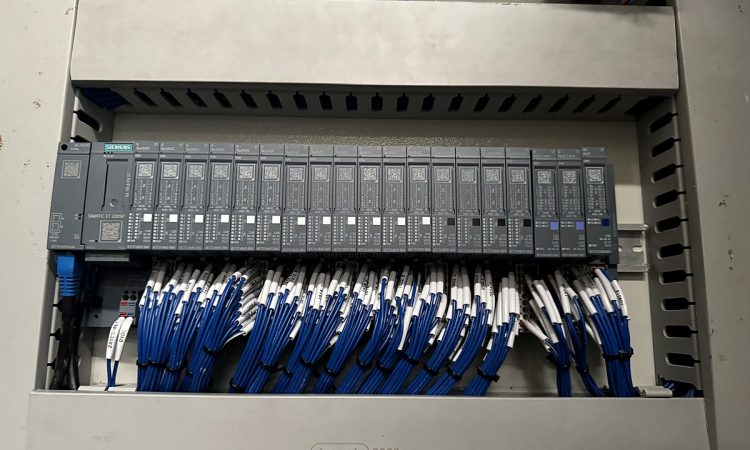
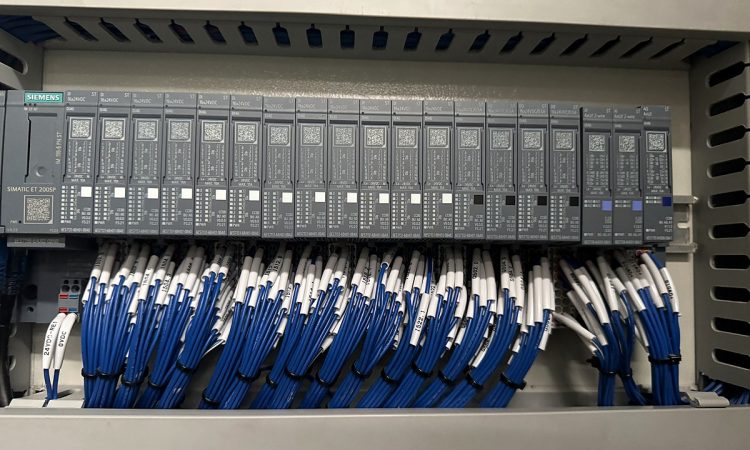
- ET 200SP distributed I/O stations
- PROFINET network with managed switches
- TIA Portal programming and version control
- WinCC HMI with alarm and trend functions
- Motor, valve and analog control function blocks
- Safety relay and interlock circuits
From Relay Logic to a Structured Program
Replacing relay and hard wired control with a structured PLC program turns the machine logic into something that can be read, tested and changed. Every motor and valve uses the same function block, so behaviour is identical across the plant and a modification made once is correct everywhere it is used.
Distributed I/O Where the Equipment Is
ET 200SP stations sit next to the equipment they serve, so field cables run metres instead of hundreds of metres back to a central panel. PROFINET carries the signals and the diagnostics together, which means a broken sensor reports itself by name instead of appearing as a dead input on a terminal strip.